7 Tips to Choose the Best Tyre Pyrolysis Machine?

Choosing the right Tyre Pyrolysis Machine is not a matter of comparing shiny photographs or the lowest quotation. It requires practical judgment, technical evidence, and careful attention to operating conditions. Feedstock moisture, tyre size, reactor design, heating efficiency, emission controls, and product quality can change the entire investment outcome. A machine that performs well in one region may struggle with another tyre mixture.

Dr. S. K. Sharma, a researcher associated with waste-tyre pyrolysis, explains, “Successful pyrolysis depends on process control, not merely on heating the tyres.” That principle should guide every evaluation. Buyers need to ask for verified capacity data, realistic oil-yield figures, energy-consumption records, and clear maintenance requirements. A factory visit can reveal more than a polished sales presentation. Look closely at weld quality, insulation, control panels, condensers, and safety systems.

Details matter.

This guide presents seven practical tips for selecting a dependable Tyre Pyrolysis Machine. It considers reactor configuration, material compatibility, environmental safeguards, automation, installation support, operating costs, and supplier experience. Compliance with applicable environmental and workplace requirements must remain non-negotiable. However, technical brochures are not perfect evidence. Some figures may reflect ideal conditions, not daily production. That is where careful questioning becomes essential. A lower purchase price may later bring higher fuel use, frequent downtime, or difficult spare-part sourcing. The best decision balances performance, safety, serviceability, and long-term value, even when the answer is less convenient.
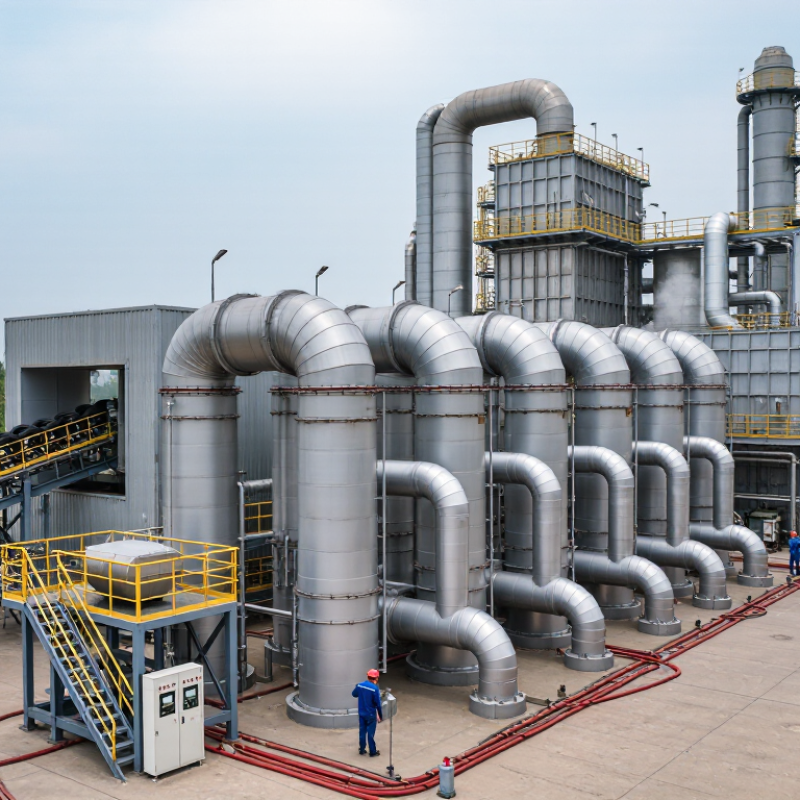
7 Tips to Choose the Best Tyre Pyrolysis Machine?

Define Your Tyre Pyrolysis Processing Needs

7 Tips to Choose the Best Tyre Pyrolysis Machine?

Define Your Tyre Pyrolysis Processing Needs

Choosing a tyre pyrolysis machine starts with your feedstock, not its advertised capacity. The WBCSD estimates that about one billion end-of-life tyres arise globally each year. Your local supply may still be seasonal, wet, or contaminated. Measure daily tyre availability, average tyre size, moisture, steel content, and storage space. A machine rated for 20 tonnes daily may perform poorly when supply falls to eight tonnes.

Be specific about your products. Do you need tyre-derived oil, recovered carbon black, or separated steel? The U.S. EPA reported about 290 million scrap tyres generated in 2019, with roughly 71.6% entering beneficial-use markets. That figure shows the importance of reliable outlets, not just production volume. Test your feedstock before selecting the reactor, condenser, and gas-cleaning system. Small differences matter.

Ask for measured data at similar operating conditions. Request oil yield, energy use, start-up time, maintenance hours, and non-condensable gas performance. Independent laboratory testing is valuable. So is a site visit. A spreadsheet can still mislead. Check whether the quoted capacity excludes downtime, tyre cutting, or final carbon processing. Confirm temperature control, pressure protection, emissions monitoring, and operator training. Local environmental requirements must shape the design. A cheaper machine may become expensive when feed preparation, residue handling, and compliance costs are added.
Compare Machine Capacity, Design, and Operating Efficiency

Choosing a tyre pyrolysis machine requires more than comparing advertised output. Start by matching capacity with your actual tyre supply. A machine rated for ten tonnes daily may perform poorly when fed only three tonnes. Measure twice.

Check whether the stated capacity reflects continuous operation or one ideal batch. Ask for cycle time, loading limits, and expected yield from your tyre type. Mixed tyres, moisture, and steel content can change results. Small details matter. Examine the reactor design, material thickness, sealing method, and access points. A well-designed chamber should support even heating and straightforward cleaning. Inspect the condenser layout too. Efficient gas cooling can reduce energy demand and improve oil recovery. Safety controls, pressure monitoring, emergency shutdowns, and emission treatment must meet local requirements.

Operating efficiency includes more than fuel consumption. Compare energy used per tonne, labour needs, warm-up time, and maintenance intervals. Ask whether waste gas can support heating without weakening process control. Review test records from similar feedstock, not only laboratory figures. Request evidence of stable operation over several cycles. One uncomfortable truth: the cheapest machine can become expensive through downtime, blocked pipes, or difficult repairs. I have seen capacity figures look impressive while actual throughput remained inconsistent. Leave room for that risk. Confirm spare-part availability, operator training, inspection access, and technical support. A practical choice balances capacity, durable design, measurable efficiency, and dependable service.

Check Heating Systems, Safety Features, and Emission Controls

Choosing a tyre pyrolysis machine requires more than checking reactor capacity. The World Business Council for Sustainable Development’s Tire Industry Project reports that over one billion tyres reach end of life globally each year. That scale makes heat stability, operator protection, and pollution control essential.

Tip 1: Check the heating system. A reliable reactor should provide even heat across the chamber, not hot spots near the burner. Ask for temperature records, fuel-use data, and independent performance tests. Electric, gas, and thermal-oil systems each have trade-offs. Lower fuel use does not always mean cleaner operation.

Tip 2: Inspect safety features closely. ISO 12100 risk-assessment principles support guarded moving parts, emergency shutdowns, pressure relief, and gas-leak detection. Look for alarms that operators can hear beside the reactor. A control screen alone is not enough. In real plants, dust and heat can make sensors unreliable, so maintenance access matters.

Tip 3: Examine emission controls, not just product yield. The European Environment Agency identifies tyre-wear particles as a major source of environmental microplastics, reminding us that waste processing needs strong containment. Request stack-test results for particulate matter, sulphur compounds, volatile organic compounds, and carbon monoxide. Condensers, scrubbers, filters, and flare systems should be sized for changing feedstock. One overlooked issue is start-up emissions. They may differ sharply from normal operation. Ask how the machine handles them.

7 Tips to Choose the Best Tyre Pyrolysis Machine? - Check Heating Systems, Safety Features, and Emission Controls

No. Selection Dimension What to Check Practical Screening Criteria Why It Matters Evidence to Request
1 Heating System and Temperature Control Confirm whether the reactor uses indirect heating, how heat is transferred, and whether temperature sensors are installed at more than one location. Preferred
Indirect heating with closed-loop temperature control, independent high-temperature cut-off, and typical tyre pyrolysis operation around 350–550°C.
Uniform, controlled heating supports more consistent oil, gas, and char production while reducing the risk of local overheating and material degradation. Request a process-flow diagram, temperature-control specification, sensor locations, heating-fuel consumption data, and a witnessed temperature-uniformity test.
2 Air Ingress and Pressure Management Check reactor sealing, flange design, rotary seals, pressure measurement, and the method used to prevent oxygen from entering the process. Look for an oxygen-limited or oxygen-free reactor, continuous pressure monitoring, controlled negative pressure, and alarms for abnormal pressure or air leakage. Uncontrolled air ingress can create fire or explosion hazards, increase oxidation, and reduce process stability. Request pressure and oxygen-monitoring points, leak-test records, seal-maintenance procedures, and the emergency response sequence for loss of negative pressure.
3 Safety and Emergency Protection Evaluate flame-failure protection, emergency shutdown, over-temperature protection, pressure relief, gas detection, grounding, and access controls. Safety functions should be independent where appropriate and should include automatic fuel shut-off, emergency-stop devices, relief protection, interlocks, and clearly documented operating limits. Pyrolysis systems handle hot solids, combustible gases, liquid hydrocarbons, and rotating equipment; layered protection reduces the consequences of abnormal conditions. Request the risk assessment, cause-and-effect chart, electrical classification, safety-instrument list, inspection schedule, and operator training records.
4 Emission Control and Monitoring Identify controls for particulate matter, smoke, volatile organic compounds, carbon monoxide, sulphur compounds, nitrogen oxides, and odour. A robust system normally includes sealed gas handling, staged condensation, particulate removal, non-condensable-gas treatment, and a flare or thermal oxidation stage where required by local rules. Emission performance depends on feedstock, operating conditions, combustion design, and local permit limits—not only on the reactor itself. Request a complete emission-control process diagram, guaranteed outlet limits, monitoring locations, sampling methods, maintenance requirements, and applicable permit assumptions.
5 Condensation and Product Recovery Review the number and arrangement of condensers, cooling-medium requirements, non-condensable-gas routing, oil storage, and pressure control. Prefer staged condensation with temperature monitoring, sealed oil transfer, vapour-tight tanks, flame arrestors where applicable, and a controlled route for remaining process gas. Effective condensation improves liquid recovery, limits vapour release, and helps prevent unstable pressure and temperature conditions. Request mass-balance data, condenser duty calculations, cooling-water or air-cooling requirements, oil recovery data, and storage-tank safety specifications.
6 Feedstock Preparation and Continuous Operation Check acceptable tyre sizes, steel and textile content, moisture tolerance, shredding requirements, feeding method, discharge design, and continuous-operation capability. The supplier should state maximum feed size, allowable moisture, feed-rate range, expected residence time, and how steel wire and hot char are removed safely. Unclear feed limits can cause blockages, uneven heating, lower throughput, excessive wear, or unsafe manual intervention. Request a written feed specification, throughput test using representative tyres, jam-clearing procedure, wear-part list, and expected availability or maintenance intervals.
7 Compliance, Maintenance, and Total Operating Cost Assess local environmental permitting, pressure-vessel requirements, electrical and fire codes, spare parts, cleaning access, energy consumption, and service support. Choose equipment supported by documented calculations, inspection certificates where required, clear maintenance intervals, accessible inspection points, and transparent utility consumption. The lowest purchase price may result in higher fuel use, downtime, compliance costs, and replacement expenses over the equipment life. Request a lifecycle cost model, guaranteed performance conditions, utility figures per tonne of tyres, spare-parts schedule, warranty terms, commissioning plan, and compliance documentation.

Note: The temperature ranges and screening criteria shown are general engineering reference points. Final equipment selection should be based on representative feedstock testing, a site-specific hazard assessment, and the emission, fire, pressure, and waste regulations applicable at the installation site.

Evaluate Product Quality and Byproduct Recovery Options

When choosing a tyre pyrolysis machine, product quality deserves careful, physical inspection. A polished brochure cannot reveal weak welds or unstable temperature control. Check the reactor material, sealing system, insulation, and automatic feeding design. Small details matter. Ask for certified material reports and complete production records. A reliable supplier should explain heat distribution, pressure protection, and emergency shutdown procedures clearly. Vague answers are warning signs.

Byproduct recovery should be measured, not simply promised. Request recent test data for fuel oil, recovered carbon material, steel wire, and non-condensable gas. Check the oil’s water content, viscosity, and possible commercial uses. Examine the recovered carbon’s ash level, particle size, and consistency. Steel should leave the process with minimal rubber contamination. Gas recovery can reduce external fuel demand, but poor cleaning may damage burners. Do not guess.

A supervised trial using similar tyre sizes can reveal more than a sales presentation. Watch the batch cycle, energy consumption, discharge temperature, and maintenance workload. Ask how often filters, seals, and condensers require replacement. One practical lesson is that recovery rates may change with tyre composition, moisture, and operator habits. That variation needs honest documentation. An attractive output figure may be unrealistic. Compare several test batches, inspect laboratory reports, and calculate recovery value against operating costs. Product quality is not only machine appearance; it is stable performance, safer operation, and repeatable byproduct quality.

7 Tips to Choose the Best Tyre Pyrolysis Machine

Evaluate product quality, operating stability, and byproduct recovery performance. The chart shows a typical mass balance from 1,000 kg of end-of-life tyres, using midpoint values from commonly reported industrial output ranges.

Selection focus: Prioritize efficient oil condensation, high carbon black and steel recovery, stable gas utilization, reliable temperature control, emissions treatment, and consistent output quality. Actual yields vary with tyre composition, moisture, feed preparation, and operating conditions.

Assess Supplier Reliability, Maintenance, and Total Costs

Choosing a tyre pyrolysis machine requires more than comparing advertised capacity. Supplier reliability should be checked through recent customer references and verified operating sites. Ask for production records using similar tyre sizes and moisture levels. A factory visit can reveal assembly quality, testing procedures, and spare-part storage. Review warranty terms carefully, especially coverage for reactors, condensers, seals, and control systems.

Maintenance determines whether the machine earns money or waits for repairs. Choose a design with accessible wear parts and clear inspection points. Confirm the expected service interval for seals, bearings, filters, and pumps. Ask how quickly technicians respond to alarms and whether remote support is available. Practical training matters. Your operators should practice safe shutdowns, cleaning, and emergency checks before production begins. Small details matter.

Calculate total costs beyond the purchase price. Include freight, installation, electrical work, permits, labor, utilities, consumables, and residue handling. Request realistic energy-use figures, not only ideal laboratory results. A common planning mistake is ignoring downtime during the first three months. Include a repair reserve in the financial model. Run a witnessed test with representative feedstock before signing final acceptance. Measure output quality, cycle time, fuel use, and emissions data. Cheap equipment can become expensive quickly. Supplier promises also need written evidence.

Whether your solution requires a single pumping application or an expansive engineered system,
CheckPoint is committed to becoming your partner in excellence.